CNC machining & assembly
You can order lengths, or you can order a part that bolts on
Most extrusion suppliers stop at a cut length. That means you receive aluminium, and the machining, the finishing sequence and the assembly become your problem — including the scrap when a hole is drilled in the wrong order. This page is the routing we run, and the one decision that changes whether a machined part is acceptable or scrap: whether the cut comes before or after the finish.
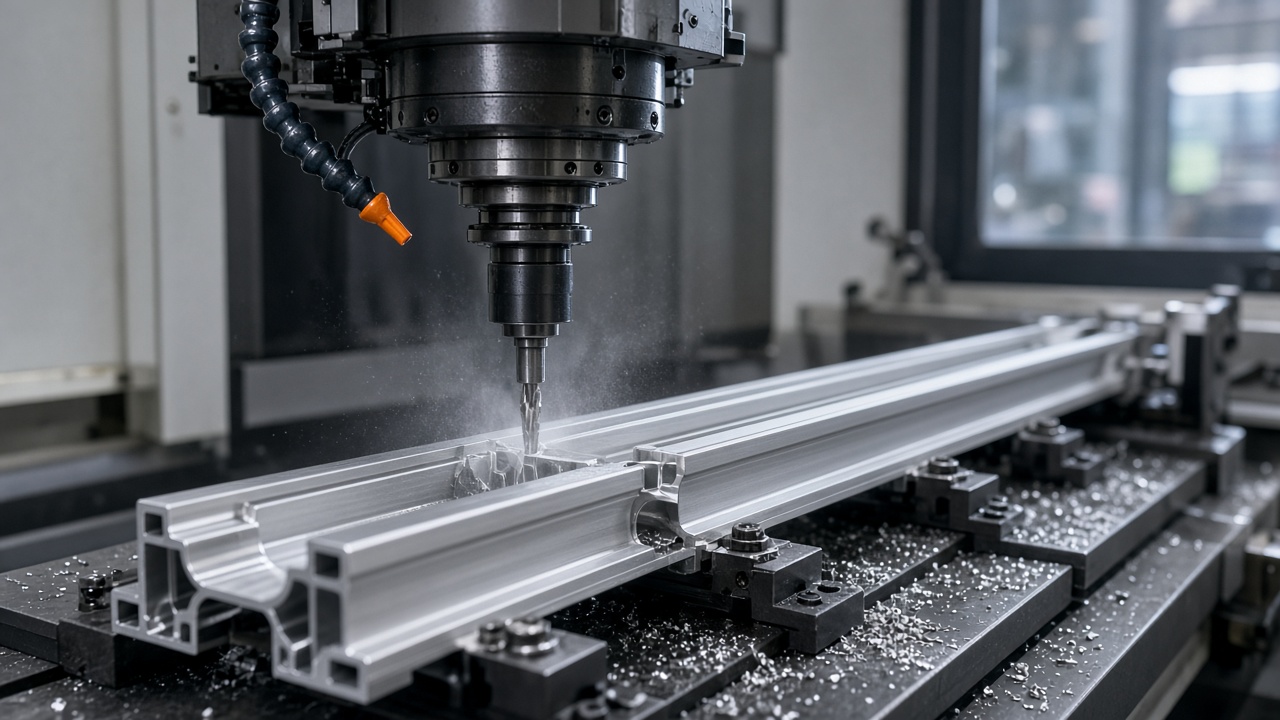
- 01Cutsaw, ±0.5 mm
- 02Machinemill, drill, tap
- 03Deburrbefore coating
- 04Finishcoat or anodize
- 05Assembleinserts, fasteners
- 06Packinterleaved
The decision
Machine first or finish first — both are used, for different reasons
There is no universally correct order. There is a correct order for each feature, and a supplier who applies one rule to the whole part will produce at least one visible defect. This is how the choice actually breaks down.
| Consideration | Machine, then finish | Finish, then machine |
|---|---|---|
| Burrs | Deburred before coating — nothing is trapped under the film | Burr breaks the coating at the cut edge, and the chip sits under the film |
| Cut faces | Fully coated — the machined face gets the same film as the rest | Bare aluminium at every cut. Fails a salt-spray review and is visible on dark colours |
| Threads and bores | Masked or plugged, then cleaned after — extra handling | Cut after coating, so thread flanks are clean metal by definition |
| Dimensional control | Film growth measured and compensated at the drawing stage | No film growth to allow for — the last operation sets the final size |
| Damage risk | Coated parts then handled through machining and assembly | Machining a coated part risks scratching the surrounding film |
| Choose it when | The part is visible, the machined faces are also visible, or the part is exterior | Threads, precision bores, or electrical contact faces must stay bare and conductive |
In practice a single part often needs both: coat the body, then machine the two features that must stay conductive, with those faces masked. That is a per-feature decision and it belongs on the drawing, not in a production meeting after the first batch.
Arithmetic buyers forget
The finish changes the dimension, so the tolerance stack is not additive in the way you expect
A machined feature does not stay the size you machined it once it has been coated. Anodizing grows roughly half the film thickness outward on each surface; powder sits entirely on top. On a tight groove or a sliding fit, this is often the whole tolerance.
- Saw cut
- Length set by the saw stop. Burr removed afterwards, so the final length is set here and nothing later changes it.
- CNC machining
- Position and size of holes, slots and pockets. Measured on the bare part, before any film.
- Anodize, 15 µm
- Grows about 7.5 µm per surface. A 10 mm bore becomes roughly 9.985 mm; a groove narrows by twice that.
- Powder, 80 µm
- Film sits on the surface. A groove 2 mm wide becomes about 1.84 mm if both walls are coated, which is usually more than the fit allowance.
- Assembly
- Press-fit inserts and fasteners add their own position error, and the joint absorbs less than the sum of the parts suggests.
±0.5 mm
±0.1 mm
+7.5 µm / face
−80 µm / face
Stack-up
If a bore or groove is tolerance-critical, say so. It gets machined after finishing, or masked, or the drawing gets a note that the dimension applies after coating — which is a different instruction from the one most drawings carry.
Scope
What we run, to what tolerance
Stated as operation and capability rather than a list of machine names, because the machine is not the constraint — the fixturing and the inspection are.
| Operation | Capability | Held to |
|---|---|---|
| Cut to length | Circular saw, deburred and chamfered if specified | ±0.5 mm on length |
| CNC milling | 3-axis, 1,200 × 600 × 500 mm envelope, single and multi-setup | ±0.1 mm standard, ±0.05 mm on request with CMM report |
| Drilling | Multi-spindle and single-spindle, position-critical patterns | ±0.1 mm position |
| Tapping | M3 to M12, through and blind | Go / no-go gauged, 100% on critical threads |
| Deburring | Automated tumbling plus manual on visible edges | No burr protruding on a coated face |
| Assembly | Press-fit inserts, fasteners, sub-assemblies, kitted by part number | Torque and position recorded per batch |
The last 5%
Packing is part of the process when the part is already finished
A coated and machined part that arrives scratched is a rejected part, and the argument about who scratched it is unwinnable. These four are the difference between a shipment that passes goods-in and one that starts a claim.
Interleaved, not bundled
Coated lengths are separated by foam or paper, not strapped metal-to-metal. Strapping marks on a matt finish are permanent.
Machined faces protected
Bare machined faces get a peelable film or a slip sheet, because they are the first thing to oxidise in transit.
Threads capped
Plugs stay in until assembly. A painted thread is a rework job, and re-tapping removes the coating anyway.
Crate marked by part number
Assemblies are kitted and labelled per part, so goods-in can check a crate against a BOM without opening every bundle.
