Die development & tooling
A die is a consumable. Price it like one, per ton.
Buyers compare die quotes as a one-off number, which is the wrong unit. A die that costs twice as much and lasts three times as long is the cheaper die. This page is the arithmetic, the point at which a die is worth repairing rather than remaking, and what we record so a re-order behaves like the first run. Including what we can save on someone else’s die — and what we cannot.
Die record
- Material
- H13
- Hardness
- HRC 48–52
- Max diameter
- 380 mm
- Min wall
- 0.8 mm
- Bearing accuracy
- ±0.02 mm
- Life, simple
- 50+ t
- Life, complex
- 15–25 t
- Lead, soft
- 5–7 days
- Lead, hard
- 10–14 days
The arithmetic
Cost per ton, and why the cheap die is not the cheap die
Divide the die price by the tons it will produce before it needs replacing, and you get the only figure that belongs in a unit-cost comparison. The multipliers below are illustrative — a real die price depends on the section — but the shape of the answer does not change.
| Scenario | Die cost | Life | Cost per ton | At 50 t / yr | At 300 t / yr |
|---|---|---|---|---|---|
| Simple solid profile | 1.0× | 50 t | 0.020× | 0.020× | 0.0033× |
| Hollow, single cavity | 1.8× | 25 t | 0.072× | 0.072× | 0.0120× |
| Wide thin-wall hollow | 3.0× | 15 t | 0.200× | 0.200× | 0.0333× |
| Spread, best to worst | 3.0× | 3.3× | 10× | 10× | 10× |
What this actually tells you: at 50 t a year, tooling is a real line in your cost sheet and die life matters as much as die price. At 300 t a year the die is almost irrelevant per ton — which is exactly when buyers over-negotiate the tooling and under-negotiate scrap rate, run speed and straightness. Those are the numbers that scale with volume.
The question buyers actually ask
Repair or remake: what can be saved on a die already running badly
Much of the die work we are asked to rescue arrives from another tool room. Some of it is recoverable in a day. Some of it is scrap metal, and telling you that on the phone is cheaper than telling you after a week of trials.
Usually fixable
- Feed imbalance — one wall running thin. Bearing lands are shortened on the fast side and the die is re-trialled.
- Twist on an asymmetric leg — often a bearing correction, occasionally a run-out table change rather than a die change.
- Die lines on a visible face — bearing polished. If the mark sits on a decorative face we will say so, because polishing buys time, not a permanent fix.
- Localised wear at a high-flow corner — welded and re-cut, then nitrided. Viable once, sometimes twice, before the geometry drifts.
- Wrong bearing length for the press it sits on — re-cut for the correct press, if there is enough land left to remove.
Not worth saving
- Wrong die type for the section — a flat die asked to make a closed hollow will never balance, whatever is done to the bearings.
- Cracked or collapsed tongue — the web is gone. Re-welding a tongue on a production die is a fatigue failure waiting for your largest order.
- No land left to correct — once the bearing has been polished and re-cut repeatedly, there is no material left to move.
- Wrong alloy assumed at design — a die cut for 6063 bearing lengths will not run 6061 at production speed, and re-cutting usually costs more than a new die.
- Heat treatment never done, or done once — the die keeps moving between runs. Re-hardening a die that has already run is a gamble, not a repair.
Send the die number, the section drawing and what it is doing wrong. We will tell you which column it falls into before you ship it to us.
Wear
What shortens die life, and which of those you control
Die life is quoted as a range for a reason. The same tool room will get 50 tons from one die and 15 from another, and the difference is usually six variables — two of which are set by your drawing.
- Wall thickness
- Thin walls need higher pressure and longer bearing contact, so the bearing wears faster. Below 1.0 mm the effect is not linear.
- Tongue and fin ratio
- Narrow tongues run hot and erode at the tip. This is the largest single life penalty on heat-sink and capping sections.
- Alloy and billet temperature
- 6061 run hot is more abrasive on the bearing than 6063. Raising temperature to gain speed trades die life for throughput.
- Nitriding interval
- Gas nitriding between runs restores surface hardness. Skipping it to save a day is the most common way a die loses half its life.
- Foreign metal in the billet
- Hard inclusions score the bearing and cannot be polished out. The spectrometer check before each run exists for this reason.
- Handling between runs
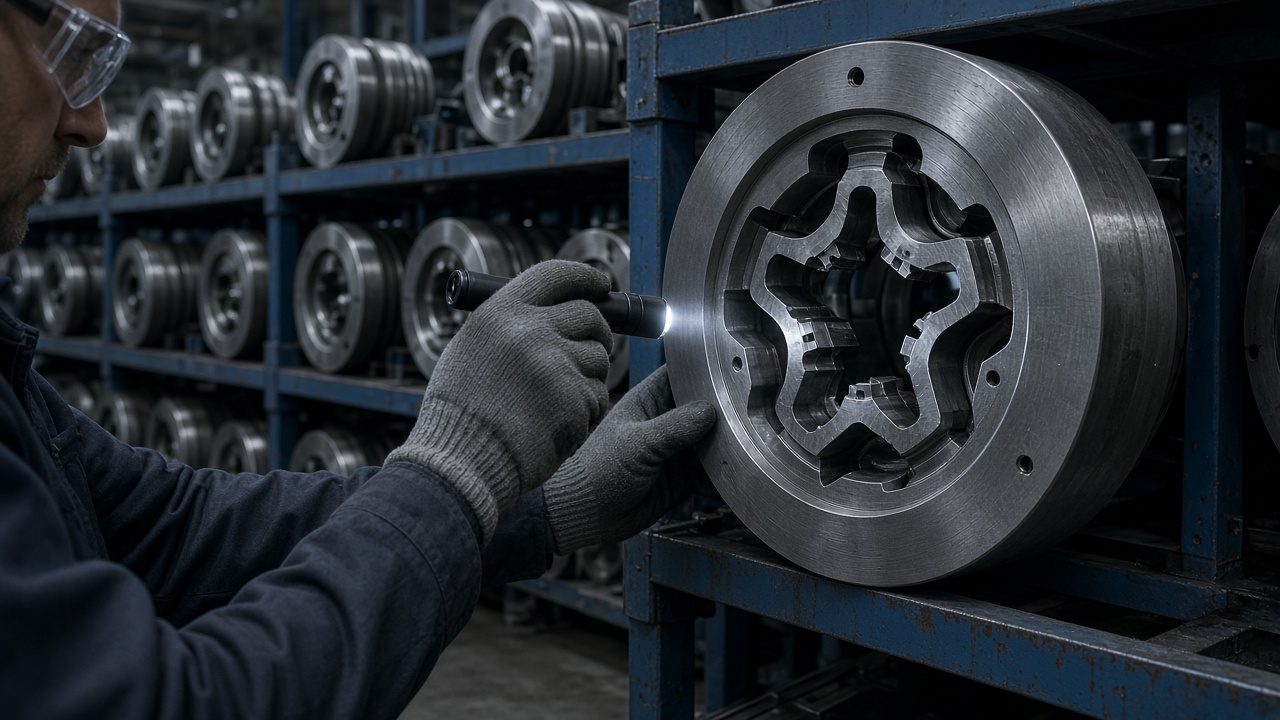
- A die dropped on a concrete floor is a die with a moved bearing. Rack storage rather than floor storage is not a detail.
Set byYour drawing
Set byYour drawing
Controlled byPress settings
Controlled byDie maintenance
Controlled byIncoming inspection
Controlled byDie store
Traceability
What is on the die card
Every die is numbered and stamped, and the card follows it for its whole life. It is the reason a re-order two years later reproduces the same section instead of starting a new trial loop.
Recorded at build
- Die number, die type, and the press it was cut for
- Section drawing revision it was cut to
- Bearing lengths per face, as cut
- Heat treatment record and measured hardness
- First-trial result: wall readings, twist, corrections made
Recorded over life
- Tons run, by date and by order
- Every correction, with the reason
- Nitriding and polishing history
- Wear pattern photographs at each service
- Remaining life estimate before the next run
Send a die number, or a section that keeps failing, and we will price the fix before you commit.
Ask about a die →