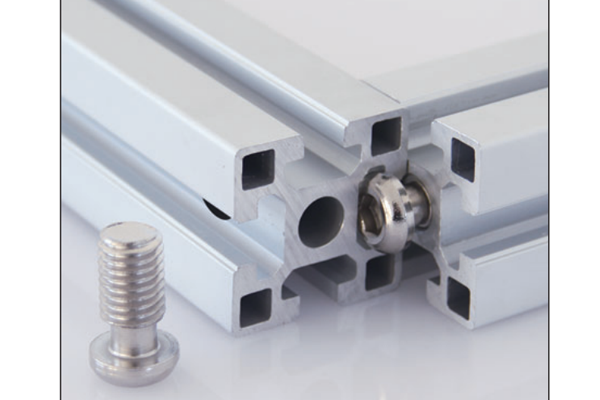
Self-Tapping Screw Connector for Aluminium Profile M6 M8 M10 to 50 mm Series
A self-tapping screw connector for aluminium profiles in M6, M8 and M10. Forms its own thread in the profile core bore for a completely hidden joint with no visible fixing.
| Material | Hardened steel, zinc plated or stainless |
|---|---|
| Alloy Grade | Hardened carbon steel, zinc plated; 304 stainless option |
| Temper | custom |
| Section Size | M6, M8 and M10 studs to suit profile core bores |
| Slot | Fits the core bore of 30, 40, 45 and 50 series profiles |
| Length | Stocked in standard lengths, custom lengths on request |
| Tolerance | ISO 965-2 thread tolerance 6g |
| Surface | Zinc plated or stainless, passivated |
| MOQ | 1000 |
| Lead Time | 12-20 days after deposit |
| Loading Port | Shanghai / Ningbo |
| Supply Ability | 5 million pieces per month |
| Payment Terms | T/T 30% deposit + 70% before shipment | L/C at sight |
| Trade Terms | FOB | CIF | EXW |
| Certifications | ISO 9001:2015 | RoHS | REACH |
Connecting elements · Threaded joints
A screw connector for aluminium profile is a hardened steel stud with a flange head that is driven into the core bore at the end of a profile and forms its own thread in the aluminium. It is made in M6, M8 and M10 and is the cheapest way to hide a joint completely: no bracket, no bolt head, no visible fixing of any kind. The stud goes into one member’s end, the second member is brought up over it, and a cross bolt through the second member locks the joint.
The one thing that decides whether this joint works or fails is the size of the hole you drill. A thread-forming screw does not cut the aluminium away, it displaces it, so the core hole has to be larger than the tapping drill you would use for a cutting tap. Drill the cutting size and the screw will seize; drill too large and it will strip. The exact figures are in the table below, and they are not the ones most people expect.
Forming a thread is not the same as cutting one
A cutting tap removes metal to create a thread. A thread-forming screw does the opposite: it pushes the aluminium aside, so the material that ends up forming the thread flanks is cold worked and slightly harder than the parent metal. In a soft alloy like 6063 that is an advantage — the formed thread is stronger than a cut one of the same size, and there is no swarf to clear from a blind hole.
The consequence is that the core hole is bigger, not smaller, than a tapping drill. For an M8 x 1.25 thread a cutting tap needs a 6.8 mm hole; a thread-forming screw needs about 7.4 mm. Drill 6.8 mm for a forming screw and it will jam and shear; drill 8.0 mm and there will not be enough material left to form a thread.
| Thread | Pitch | Cutting tap drill | Thread-forming core hole | Difference |
|---|---|---|---|---|
| M6 x 1.0 | 1.0 mm | 5.0 mm | approx. 5.5 mm | +0.5 mm |
| M8 x 1.25 | 1.25 mm | 6.8 mm | approx. 7.4 mm | +0.6 mm |
| M10 x 1.5 | 1.5 mm | 8.5 mm | approx. 9.2 mm | +0.7 mm |
Use the forming hole, not the tapping drill. This is the single most common cause of a failed screw connector installation. The two holes differ by half a millimetre, which is nothing until the screw seizes halfway in with no way to back it out.
Engagement decides the strength
A thread in aluminium needs more engagement than the same thread in steel, because the aluminium is what shears. The working rule is one diameter of engagement as an absolute minimum and one and a half diameters for full strength. Below one diameter the thread strips before the bolt breaks; above one and a half diameters extra depth adds nothing.
| Thread | Minimum engagement (1 x d) | Full strength (1.5 x d) | Torque ceiling in aluminium |
|---|---|---|---|
| M6 x 1.0 | 6 mm | 9 mm | approx. 8 N m |
| M8 x 1.25 | 8 mm | 12 mm | approx. 15 N m |
| M10 x 1.5 | 10 mm | 15 mm | approx. 28 N m |
Compare those torque figures with what the same bolt would take in a steel thread — about 10 N m for M6, 25 N m for M8 and 49 N m for M10 — and you can see that the joint is limited by the aluminium, not by the fastener. Torque a screw connector to its steel value and it will strip the formed thread out of the profile.
The cheapest hidden joint, and the least re-usable
Every time the joint is taken apart and re-made, the forming screw removes a small amount of material from the thread it created. The first assembly is strong, the second is nearly as good, and by the fifth the thread is loose. That behaviour is inherent to the design and no amount of care changes it.
| Assembly cycle | Thread condition | What to do |
|---|---|---|
| First assembly | Full formed thread, full torque | Torque to the ceiling in the table above |
| Second and third | Thread still sound, slight loss of grip | Reduce torque by about 20 per cent |
| Fourth and fifth | Thread visibly worn, joint may creep | Acceptable for a light non-structural joint only |
| Beyond five | Thread stripped or loose | Re-drill oversize and use a threaded insert, or move to a new joint type |
The practical conclusion is that a screw connector belongs on a frame that is assembled once and then left alone — a production machine, a fixed guard, a conveyor frame that will not be modified. It does not belong on a prototype, on a frame that will be re-configured, or on a joint that has to be re-torqued during commissioning. For those, use an end face connector or a bracket, both of which can be taken apart indefinitely.
Installing a screw connector
- Drill the core hole to the forming size, not the tapping size Use the middle column of the first table. Drill the hole square to the end face and deburr the mouth.
- Drive the stud in one continuous pass A forming screw should go in without stopping. Stopping and restarting damages the thread that has already been formed.
- Stop when the flange seats on the end face The flange is the depth stop. If it will not seat, the hole is undersize and forcing it will shear the stud.
- Bring the second member over the stud and fit the cross bolt Check the joint is square before tightening the cross bolt, because once it is tight the position is fixed.
- Torque to the aluminium ceiling Use the torque figure from the table, not the bolt’s steel rating. The aluminium thread is what fails.
Frequently asked questions
Can I use an ordinary bolt instead of a screw connector?
No. A standard bolt needs a pre-cut thread, and drilling and tapping a deep core hole in a long profile is not practical on site. The screw connector exists precisely so that the thread can be formed at assembly.
Will it work on an anodised profile?
Yes. The forming screw cuts through the anodised layer at the bore, which is a few tens of microns thick. It does mean the thread is formed in bare metal and is not protected from corrosion, so use it indoors or add a sealing compound in wet environments.
What happens if the thread strips?
Re-drill the bore oversize and fit a threaded insert, which gives you a steel thread and a joint that can be dismantled many times. That is the standard repair and it leaves the member usable.
Which size should I choose?
Match the stud to the profile’s core bore. Use M6 for 30 series, M8 for 40 series and M10 for 45 and 50 series. Going larger than the core bore allows is not possible; going smaller wastes capacity.
Do you supply the studs with the drill size marked?
Yes. Studs are bagged by size with the forming core hole diameter and the torque ceiling printed on the label, so the installation data travels with the parts.
Send the series and how often the joint is opened
Tell us the profile series and whether the frame will be re-configured. We will confirm the stud size and core hole, and supply the forming data with the parts.
Request a QuoteRelated Products
 End Face Connector for Aluminium Profile M8 M10 up to 50 mm Series with Spring Clip
An end face connector for aluminium profiles in M8 and M10 with a spring…
 Aluminium Profile Shelf System 40×40 mm T-Slot Uprights for Workshop Racking
A bolted aluminium profile shelf system in 40 x 40 mm T-slot uprights and…
Aluminium Framing Extrusion Kit 40×40 mm 40 Series Cut List for Machine Frames
A cut-to-length aluminium framing extrusion kit in the 40 series: profile cut to a…
 Miter Connector Model C 90 Degree Corner Joint for 40 mm Aluminium Profiles
Miter connector Model C for 90-degree corner joints on aluminium T-slot profiles. Internal tie…
 Oblique Connector Model C Angled Joint for 40 mm Aluminium Profiles
Oblique connector Model C for adjustable-angle joints on aluminium T-slot profiles. Internal tie rod,…
 Oblique Connector Model P Angled Joint with Panel Face for 40 mm Aluminium Profiles
Oblique connector Model P with panel mounting face for angled joints on aluminium T-slot…
 Aluminium Angle Extrusion 40x40x5 mm for Frame Assembly and Bracing
40 x 40 x 5 mm aluminium angle extrusion in 6061-T6 for frame assembly…
 Aluminium Extrusion Profile Supply: 15 to 45 Series Kits, 8 mm Slot
Aluminium extrusion profile supply for Ahmedabad in 6063-T5: electrical cabinet frames with a designed…
