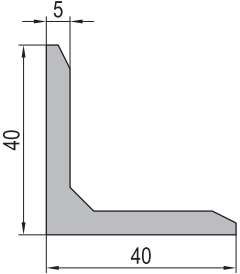
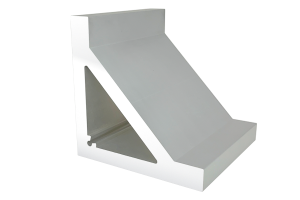
Aluminium Angle Profile 40 x 40 x 5 mm Solid Equal Leg Corner Section
Equal leg 40 x 40 x 5 mm extruded aluminium angle at about 1.01 kg/m with an R3.5 heel. Supplied in 6063-T5 for visible trim or 6061-T6 where the angle carries load or is welded.
| Material | Aluminium |
|---|---|
| Alloy Grade | 6063-T5 for appearance, 6061-T6 for load |
| Temper | T5 |
| Section Size | 40 x 40 x 5 mm |
| Slot | Not applicable, this is a solid equal leg L section with no slot |
| Length | 6 m stock, cut to drawing to +/-0.5 mm |
| Tolerance | EN 755-9 / GB/T 6892, wall +/-0.15 mm |
| Surface | Mill finish / clear, champagne, bronze, black or brushed anodised |
| MOQ | 800 m |
| Lead Time | Typically 20 to 32 days after deposit, longer for a colour matched anodised batch |
| Loading Port | Shanghai, Ningbo, Qingdao |
| Supply Ability | Extrusion, cutting, machining and anodising in house |
| Payment Terms | T/T 30 per cent deposit, balance against copy of bill of lading; L/C at sight for larger orders |
| Trade Terms | FOB, CIF, CFR, EXW |
| Certifications | ISO 9001:2015, EN 755-9, RoHS and REACH declarations |
01What is a 40 x 40 x 5 mm equal leg angle?
What makes it different from a T-slot profile?
It has no slot at all. Both legs are solid 5 mm aluminium, joined at a heel with an R3.5 internal radius. That means you cannot slide a nut into it, and in exchange you can drill, tap, weld, notch and bend it anywhere along its length. It is a piece of structural trim rather than a framing member.
When is the solid angle the right choice?
When the angle is doing one of three jobs: covering a corner, carrying a modest load across a short span, or giving you somewhere to drill that a hollow section cannot. If you need to bolt accessories onto it at arbitrary positions later, buy a slotted section instead.
Why is there a choice of alloy?
6063-T5 gives the better surface and is the standard choice for trim that will be seen and anodised. 6061-T6 has roughly double the yield strength and is weldable, so it is the choice when the angle carries load or is welded into an assembly. The two look the same in section and differ in what you are allowed to do with them afterwards.
02Section data
| Item | Value | Note |
|---|---|---|
| Envelope | 40 x 40 x 5 mm | equal leg L section |
| Leg thickness | 5 mm | nominal, both legs equal |
| Cross-section area | approx. 375 mm2 | two legs less the overlap at the heel |
| Heel radius | R3.5 | internal; larger radii available on request |
| Second moment of area | approx. 5.6 cm4 | about an axis parallel to a leg |
| Section modulus | approx. 2.0 cm3 | to the outer face of the heel |
| Weight | approx. 1.01 kg/m | a 6 m bar is about 6.1 kg |
| Alloy | 6063-T5 or 6061-T6 | appearance or load |
| Finish | mill, anodised or brushed | 10 to 20 micron anodising |
| Standard | EN 755-9 / GB/T 6892 | wall tolerance +/-0.15 mm |
| Length | 6 m stock | cut to drawing to +/-0.5 mm |
The section modulus of about 2.0 cm3 is the number to compare against when you are deciding whether this angle can carry a load. A 40 x 40 mm slotted profile of a similar weight has roughly twice that figure, because a closed box puts its material further from the neutral axis. The angle wins on machinability, not on stiffness.
03Solid angle against slotted profile: the real trade
The comparison that matters is not strength per kilogram. It is what you are allowed to do to the section after you buy it.
A slotted profile gives you a fixing system. You slide nuts in, you bolt things on, you take them off again, and you do it without making a single hole. That is enormously valuable on a machine frame, and it is why every framing range is built around slots.
A solid angle gives you material. You can drill a 10 mm hole at 137 mm from one end because that is where the bracket has to go. You can countersink it, tap it, weld a gusset into the heel, or cut a notch so it passes over a rib. None of those are possible on a hollow section without plugging it first.
And the angle gives you a flat back. Both legs sit flush against the two faces of a corner, which is exactly what a capping or an edge trim has to do. A square hollow section cannot do that: it presents a corner to the corner.
| Requirement | Solid 40 x 40 x 5 angle | Slotted 40 x 40 profile |
|---|---|---|
| Fix anywhere along the length | yes, drill and tap | only at the slot |
| Reposition a fixing later | no, the hole stays | yes, slide the nut |
| Weld into an assembly | yes in 6061-T6 | not recommended |
| Sit flush into a corner | yes, both legs flat | no, presents a corner |
| Stiffness at equal weight | lower, about 5.6 cm4 | higher, roughly double |
| Take a bolted accessory kit | no | yes, the whole series fits |
| Visible architectural edge | yes, the intended use | looks industrial |
| Cost per metre | lower | higher |
Read down that table and the decision is usually obvious. If your requirement list is made of the left hand column, buy the angle. If it is made of the right hand column, buy the profile. The only genuinely difficult case is a member that has to be both stiff and fixable, and for that the answer is usually a slotted profile with an angle bolted to it.
04Choosing the alloy: 6063-T5 against 6061-T6
6063-T5, the appearance alloy
- The angle is seen: architectural trim, shopfronts, reveals
- It will be anodised to a decorative finish
- It will be brushed or given a colour matched anodised finish
- Loads are light: the trim carries itself and a panel
- It will be cut and mitred, not welded
- The best surface finish for the money is what matters
6061-T6, the load alloy
- The angle carries a real load or spans a gap
- It will be welded into a fabricated assembly
- It will be drilled and tapped heavily along its length
- It works at elevated temperature or outdoors under load
- The finish is secondary: paint, or mill left as is
- Yield strength is the governing number, not appearance
The practical consequence: if you order 6063-T5 and then weld it, you have annealed the heat affected zone and lost most of the temper. If you order 6061-T6 and then ask for a bright decorative anodise, the surface will show the alloy’s coarser grain and will not match a 6063 trim run. Decide which one matters before you order, not after.
05Failure modes to design out
| What goes wrong | Why it happens | Design it out by |
|---|---|---|
| Angle springs open at the heel | an extruded angle has residual stress and is not a stiff shape in torsion | clamp both legs during welding, and use a gusset at any loaded corner |
| Hole elongates under load | a 5 mm leg gives a thin bearing surface for a bolt | add a washer or a backing plate, or move the fixing to a gusset |
| Anodised faces chip on the cut ends | cut ends are bare aluminium and are the first thing knocked | specify end caps, or order cut lengths with a deburred and anodised end |
| Galvanic corrosion at the fixing | steel screws into aluminium in a damp location | use stainless fasteners with a nylon washer, or isolate with a gasket |
| Colour mismatch against an existing run | a top-up order was anodised in a different batch | order the whole job in one anodising run, or accept a written colour tolerance |
06What to check before you order
Procurement checklist for the 40 x 40 x 5 mm angle
- Confirm the alloy: 6063-T5 for visible trim, 6061-T6 for load or welding. This is the single most common specification error on this section.
- Confirm the heel radius. R3.5 is standard; larger radii are a different die and a longer lead time.
- Confirm the cut list and the end treatment: square cut, mitred, deburred, or drilled to a hole pattern.
- Confirm the finish: mill, clear anodised, champagne, bronze, black, or brushed.
- Confirm whether the ends need sealing or capping if the angle is used outdoors.
- Confirm the fixing method and that the fasteners are compatible with aluminium if the installation is damp.
- Confirm the quantity in metres and allow for mitre waste: a 40 mm leg cut at 45 degrees loses 40 mm per end.
07Terms used on this page
- Equal leg angle
- An L section whose two legs are the same length. It loads symmetrically and its principal axes run at 45 degrees to the legs.
- Heel
- The inside corner where the two legs meet. Its radius is set by the die and is the detail the eye reads on visible trim.
- Section modulus
- Second moment of area divided by the distance to the extreme fibre. It converts directly into the bending moment a section can take.
- Gusset
- A flat plate welded or bolted across an angle corner to stop the legs springing apart under load.
- 6063-T5
- The standard architectural extrusion alloy. Good surface, moderate strength, not normally welded.
- 6061-T6
- A higher strength, weldable alloy used where the section carries load. Coarser surface, so less suited to bright trim.
08Questions buyers ask
Can the angle be welded?
Yes in 6061-T6, which is the alloy to specify if welding is part of the fabrication. 6063-T5 can be welded but loses temper in the heat affected zone, so it is not specified for welded work.
Can holes be drilled and tapped anywhere?
Yes. Both legs are solid 5 mm material, so a hole can go wherever the drawing puts it. Countersinking for a flush screw head is standard.
How does it compare with a 40 x 40 slotted profile on strength?
The slotted profile is stiffer at a similar weight, roughly double the second moment of area, because a closed box puts material further out. The angle wins on machinability, weldability and its ability to sit flush into a corner.
What is the weight per metre?
Approximately 1.01 kg/m, so a 6 m stock length is about 6.1 kg.
Is it available in colours?
Clear, champagne, bronze and black anodised are standard, and brushed is available on request. Colour matched batches need a longer lead time.
Can it be supplied mitred for corners?
Yes. Mitre cutting on CNC centres is a standard operation and the mitred ends are deburred before packing.
What we need to quote this section
- The alloy and temper: 6063-T5 or 6061-T6.
- The cut list with lengths, mitre angles and any hole pattern.
- The hole details: diameter, countersink, tapping, and positions from a datum.
- The finish: mill, clear, champagne, bronze, black anodised or brushed.
- Whether the ends need deburring and protection for an outdoor installation.
- The quantity in metres or pieces.
Quotations are broken out into extrusion, cutting and mitring, machining, finish and packing, so you can see which step is driving the cost on a trim order. Browse the full aluminium profile catalogue and the angle profiles range for related sections.
Specifying aluminium angle for trim or for load?
Send the alloy, the cut list and the finish. We quote extrusion, mitring, machining and anodising as separate lines.
Request a quotationRelated Products
 Aluminium Angle Profiles Equal Leg Corner Sections 20 to 100 mm
Equal leg aluminium angle profiles from 20 x 20 mm to 100 x 100…
 Aluminium Angle Profile Bracket 100 x 100 x 15 mm Heavy Duty Corner
100 x 100 x 15 mm heavy duty aluminium angle bracket with round fixing…
 Aluminium Angle Profile Bracket 50 x 50 x 9 mm Medium Duty Corner
50 x 50 x 9 mm medium duty aluminium angle bracket with equal legs…
 Die Cast Bracket for 20 to 50 mm Series Aluminium Profiles Corner
Die cast zinc alloy corner bracket for 20, 30, 40, 45 and 50 series…
 Extruded Aluminium Angle Profile 20 to 100 mm 6061 T6 Equal Leg
Extruded aluminium equal leg angle from 20 x 20 x 3 mm to 100…
 Aluminium Angle Extrusion 40x40x5 mm for Frame Assembly and Bracing
40 x 40 x 5 mm aluminium angle extrusion in 6061-T6 for frame assembly…
 Custom Aluminium Extrusion Profile 20 to 100 mm, 6063-T5
Aluminium extrusion profiles supplied to Canada in 6063-T5 and 6061-T6, mill or anodised, with…
 Aluminium Extrusion Manufacturing Factory: 20 to 100 mm Profiles
Aluminium extrusion profiles for Gujarat, India, in 6063-T5 and 6061-T6, with anodising film selected…
