Industrial Aluminium Extrusion: Five Advantages and the Conditions Attached to Each
The standard list of extrusion benefits is accurate the way a headline is accurate. Every advantage is real, and every one carries a condition. The conditions are what decide whether the material is right for a particular job.
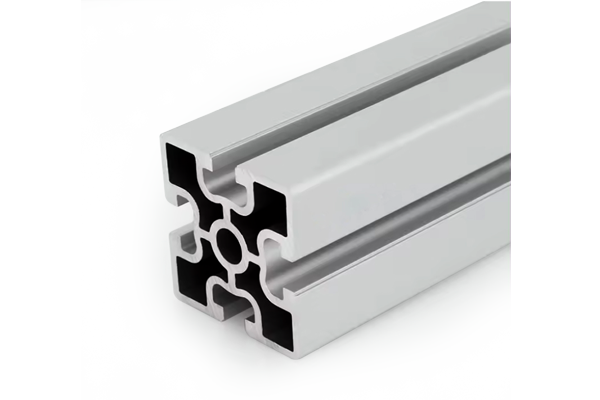
Short answer
The five claims are true and each needs a condition attached. Aluminium is about one third the density of steel, so the same section is roughly two thirds lighter, but its elastic modulus is also about one third, so the specific stiffness of the two materials is nearly identical and a stiffness-governed part saves far less mass than the density ratio suggests. The process really is shorter, provided the design does not need a machined face or a precise hole pattern. The labour saving is real and it is mostly option value rather than hours. Extrusion gives a constant cross-section to a tolerance, not a flat surface. And the corrosion resistance is conditional, because aluminium is attacked at both ends of the pH scale and needs a coating in most real environments. Aluminium wins clearly on strength-to-weight. It does not win on stiffness-to-weight, and that is the distinction that decides most machine-frame projects.
The claims are true and incomplete
Marketing lists about extrusion tend to make the same five claims: fewer process steps, reusable material, labour savings, precision, and light weight with corrosion resistance. None of them is false. The problem is that each one is stated without the condition that makes it apply, and the condition is where the engineering decision lives.
The most consequential example is weight, because it is the claim buyers repeat most often and the one that most often fails to survive contact with a real design. So it is worth working through properly.
Advantage one: mass, and the correction that changes the answer
Aluminium has a density of about 2.70 grams per cubic centimetre against roughly 7.85 for steel. That is the source of the familiar claim: for the same section, aluminium is about two thirds lighter. It is correct, and it is the wrong comparison for most machine frames.
Aluminium’s elastic modulus is around 70 gigapascals against roughly 210 for steel. Stiffness scales with the modulus, so an aluminium member of the same shape and size deflects about three times as much as a steel one under the same load. Buyers who compare weight for the same section are comparing a stiff part with a flexible one.
The honest comparison is weight for the same stiffness. Because the density ratio and the modulus ratio are almost the same number, the specific stiffness of the two materials, which is the modulus divided by the density, comes out within a few per cent of each other. Scale a steel section geometrically until its aluminium equivalent has the same stiffness, and the aluminium version lands at roughly eighty per cent of the steel mass rather than the thirty-five per cent the density ratio implies.
That still leaves a genuine advantage, and there is a second one that matters more. Extrusion can put material where it is needed, in deep hollow sections and ribs, at a cost that no steel fabrication process can match. So a well-designed aluminium extrusion does beat a steel section of the same stiffness, and most of the gain comes from the shape rather than from the material.
Where mass genuinely governs, which means anything that is lifted, moved, shipped or accelerated, the advantage is large and immediate. Where stiffness governs a long span, the advantage largely disappears.
| Property | Aluminium | Steel | Consequence |
|---|---|---|---|
| Density | approx. 2.70 g/cm³ | approx. 7.85 g/cm³ | Same section is about two thirds lighter |
| Elastic modulus | approx. 70 GPa | approx. 210 GPa | Same section is about three times as flexible |
| Specific stiffness | approx. 26 | approx. 27 | Nearly identical: little gain where stiffness governs |
| Specific strength | Markedly higher | Lower | A clear win where strength governs |
Advantage two: fewer process steps and less labour, with two conditions
The process claim is sound. An aluminium frame is designed, cut and drilled, and assembled. A welded steel frame is cut, welded, ground, and then usually painted or galvanised. The extrusion route removes welding, grinding and surface finishing, and it removes the distortion that welding introduces, which is a real and often underrated benefit because a welded frame needs straightening after fabrication.
The first condition is that the design must not need a machined face or a precise hole pattern. Extrusion gives a constant cross-section; it does not give a flat, square end, a flat face, or a hole in a defined position. Those are machining operations, they cost money, and a design that needs many of them loses much of the process advantage.
The second condition is volume. Welded steel has no connector hardware at all: the joint is the material. A bolted aluminium frame has brackets, nuts and fasteners at every corner, and the connector count rises as the section gets smaller. On a high-volume, never-changed product, that hardware bill can exceed the labour it saves. The bolt-together frame wins on labour and loses on parts.
One further point belongs here, and it is rarely mentioned: welding aluminium is not the same as welding steel. A welded aluminium joint loses strength in the heat-affected zone unless the assembly is re-heat-treated, which is impractical for a large frame. That is a strong argument for bolted construction on aluminium, and it is a material fact rather than a preference.
Advantage three: precision, and precision of what
The precision claim needs to be separated into two very different things, because suppliers often quote the better one.
An extrusion holds a cross-sectional profile to a tolerance along its whole length. That is genuinely valuable: every cut length matches, and a slot runs straight for six metres. It is also what makes the modular system work.
An extrusion does not give a machined flat face, a square cut end, or an accurately positioned drilled hole. Those come from a machining operation with its own tolerance, and they are usually what actually determines whether a frame assembles squarely. On a large frame the accumulated error from cut length tolerance is what makes a rectangle into a parallelogram, and no amount of profile precision removes it.
So the useful question on a precision claim is: precise in which direction, and to what figure, and how is it verified. A profile tolerance and a cut-length tolerance are different numbers and only one of them appears in the sales literature.
Advantage four: corrosion resistance without a coating, conditionally
The natural oxide layer is a genuine advantage: it forms immediately, it reforms if damaged, and it is the reason aluminium does not rust. It is also thin, easily damaged, and attacked at both ends of the pH scale.
The practical version of this claim is that aluminium needs no coating, which is true in a dry, neutral indoor environment and false in most others. Alkaline cleaners and fresh concrete attack it. Chlorides pit it. A cut end has no coating at all, whatever the profile was finished with.
So the advantage is real but it converts into a coating specification as soon as the environment is anything other than benign. That is not a weakness of aluminium; it is a cost line that belongs in the comparison from the start rather than being discovered later.
Advantage five: reusability, the one that compounds
The fifth advantage is the least quantified and often the most valuable: an aluminium frame comes apart and goes back together as something else. A welded steel frame does not.
This is not a sustainability slogan, it is a cash flow argument. Where a production line is expected to be reconfigured, the option to rebuild rather than replace has a value that is easy to underestimate at the quotation stage and easy to recognise three years later. It also changes the nature of the risk: a change in the process becomes a rebuild rather than a capital project.
The condition attached to it is that the frame has to be designed for disassembly. Concealed connectors that cannot be reached, joints that were torqued to a figure that damages the slot, and locking elements that cannot be re-used all reduce the option to zero. A frame that is technically reconfigurable and practically not is the worst of both worlds.
Where aluminium extrusion loses outright
Being clear about this is more useful than another list of benefits, because these are the cases where the material should not be chosen at all.
| Situation | Why aluminium loses | Better answer |
|---|---|---|
| Stiffness-critical long span | Modulus is one third of steel’s and specific stiffness is the same | Steel, or a much deeper aluminium section, or more supports |
| Elevated temperature | Strength falls progressively well below melting point | Steel, or protection and a de-rated design |
| Abrasion or wear surface | The material is soft and wears | Steel inserts, wear strips, or a hard-anodised surface |
| Repeated load cycles | No fatigue limit: life must be assessed, not assumed | Fatigue design with a load spectrum, or steel |
| Contact with steel when wet | Galvanic couple, with the aluminium corroding | Isolation, coatings, or a compatible fastener system |
| Sound reduction | Light structures transmit sound rather than blocking it | Mass, damping, or a different construction |
| Cost per kilogram | Material cost per kg is normally higher than steel | Compare installed cost, not material cost |
The break-even, and what to send with an enquiry
The comparison that decides most projects is installed cost over the life of the assembly, not cost per kilogram. That means material, machining, connector hardware, assembly labour, finishing, and the expected number of reconfigurations. In a stable, high-volume product with a long service life and no changes, welded steel usually wins. In a low-volume, frequently changed environment, aluminium extrusion usually wins by a margin that surprises people, because the reconfiguration cost of steel is not a repair, it is a replacement.
RFQ checklist — material and process choice
- What governs: strength or stiffness — state it, because it decides whether the mass advantage applies.
- Load and deflection limit — the deflection limit is the number that sizes most frames.
- Service temperature — and whether it is sustained or occasional.
- Expected number of reconfigurations — this is the option value, and it is usually the deciding factor.
- Annual volume — it determines whether a welded alternative becomes competitive.
- Machining content — flat faces, drilled patterns and tapped holes are extra operations, not profile features.
- Environment and finish — and the coating class, if the material will not be used dry and neutral.
- Installed cost basis — ask for the comparison to include hardware, labour and finishing on both options.
Ask one question before comparing: is this part limited by strength or by stiffness. If the answer is stiffness, most of the weight advantage is gone before the comparison starts.
Five ways the benefits get overstated
Related on this site
- Aluminium vs steel machine frames: choose by deflection— the stiffness comparison worked through
- Modular components: the real cost structure— where the system saves and where it costs
- Standard vs custom extrusion: the break-even— when a new die pays for itself
- What each feature on the section drawing costs— the cost of precision, feature by feature
Terms used in this article
- Specific stiffness
- Elastic modulus divided by density; the property that governs mass for a stiffness-limited part.
- Specific strength
- Strength divided by density; the property that governs mass for a strength-limited part.
- Heat-affected zone
- The region around a weld where the material’s properties have been altered by heat.
- Section modulus
- The geometric property governing bending stress in a beam; increases with depth more slowly than stiffness does.
- Option value
- The worth of being able to change a design later without replacing it.
- Installed cost
- Total cost including material, machining, hardware, assembly and finishing, rather than material cost alone.
Questions buyers ask
Is aluminium really two thirds lighter than steel?
For the same section, yes, because the density ratio is about one to three. For the same stiffness, no: the modulus ratio is also about one to three, so the specific stiffness of the two materials is nearly identical.
Then why use aluminium at all?
Because it wins clearly on strength-to-weight, because extrusion can create efficient deep sections cheaply, because it needs no welding or finishing in many cases, and because the frame can be rebuilt instead of replaced.
Does a bolted frame save labour compared with welding?
Usually yes on assembly and on rework, but the comparison has to include the connector hardware at every joint. At high volume with a stable design, welded steel can be cheaper overall.
Can aluminium be welded instead?
It can, and the joint loses strength in the heat-affected zone unless the assembly is re-heat-treated, which is impractical on a large frame. That is a strong argument for bolted construction.
When is aluminium the wrong choice?
Stiffness-critical long spans, elevated temperatures, abrasion surfaces, high-cycle fatigue duty, sound reduction, and anything in permanent wet contact with steel.
Tell us what governs the part
Say whether the design is limited by strength or by stiffness, how often it will be rebuilt and at what volume, and we will give you the comparison on an installed cost basis rather than a material cost basis.
Request a quoteRelated reading
Twelve more engineering notes from this blog, picked for this article — plus every category below.
 ApplicationsAluminium Profile for LED Strips: A Heat Sink First, a Housing Second
 Engineering DesignWhat Is a 2020 Aluminium Profile? (Weight, Slot and Load)
 Engineering DesignHow to Choose the Right T-Slot Aluminium Profile Size
 Engineering Design3030 vs 4040 Aluminium Profile: Which for Your Frame
 Materials and Engineering6063-T5 Aluminium Profile: What the Designation Actually Guarantees
 Engineering Design3030 vs 4040 Aluminium Profile: A Decision With Numbers
 Materials and EngineeringAluminum Extrusion Tolerances: How to Write a Specification Your QC Team Can Actually Inspect
 Sourcing and ProcurementDistributor Terms: Territory, Margin and Price Protection
 ApplicationsAluminium Workstations: From Fixed Benches to Reconfigurable Cells
 Engineering DesignAluminium Profile Max Span: Deflection Table by Section
 Engineering DesignWhat Your Extrusion Drawing Must Show (and What Costs You Money)
 Quality and InspectionAluminium Profile Finishes: Choose by Failure Mode, Not by Process Name
