Modular Aluminium Components: Where the System Saves Money and Where It Costs You
Modular T-slot framing is sold as a way to cut build time. That is true, but it is only half the ledger. The other half sits in the interface parts — the connectors, nuts and brackets that nobody prices until the second rebuild.
Short answer
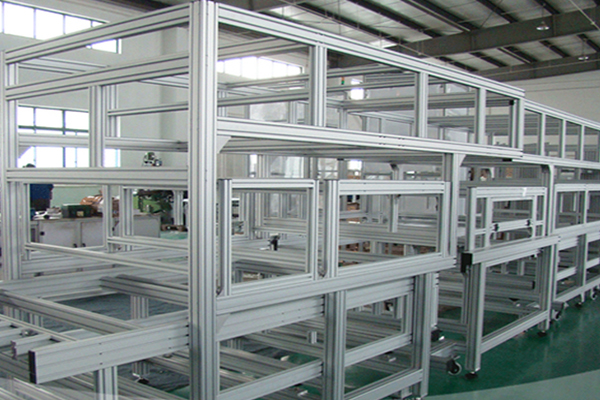
A modular aluminium profile system saves money in design hours, rework and assembly labour, and costs money in interface hardware. In a typical machine frame, extrusions account for roughly 55–70% of material spend while connectors, nuts, bolts and end caps take the remaining 25–40%. The system wins when the frame will be changed; it loses when the design is frozen and the volume is high, because a welded or a dedicated custom extrusion removes that interface premium.
The three lines on the ledger, and only one of them is quoted
When a buyer asks two suppliers for a quote on the same frame, both quotes list the extrusions by the metre and both list a hardware line. The extrusion line is easy to compare because it is length times a published kilogramme rate. The hardware line is where the comparison collapses, and the reason is structural rather than commercial.
Every node in a T-slot frame is an interface. A node consumes a connector, two to four fasteners, and the labour to seat all of it. A four-leg bench with a mid rail has more than twenty nodes. Multiply that by the hardware unit cost and the interface line stops looking like an accessory and starts looking like a second material budget.
The third line — labour and engineering hours — is the one that never appears on a quotation at all. It is also the line where modular framing wins by the widest margin, and it is the reason the system exists.
Where the money goes in a typical modular frame
- Extrusion, by metre and by wall thickness55–70%
- Interface hardware: connectors, nuts, bolts, caps25–40%
- Cutting, machining, anodising8–15%
- Engineering hours (design, drawing, revision)Not quoted
Why the ranges are wide
The interface share is not a constant. It scales with node density, not with frame size. A long, simple guard rail with four posts has a low interface share; a compact workstation with shelving, a back panel and a monitor arm has a high one, because every added function adds nodes without adding metres.
Why interface hardware costs what it costs
A connector is a small part with an unforgiving tolerance burden. It has to locate in a groove whose mouth width is held to a fraction of a millimetre, it has to clamp without deforming the extrusion wall, and it has to do both after anodising has added a few microns to every surface it touches.
That last point is the one buyers miss. Anodising is not a cosmetic afterthought in a modular system; it changes the fit. A hard anodised layer of 25 micron on both groove faces removes 50 micron of clearance from a slot, and the parts that still have to slide in that slot were toleranced before the layer existed.
The practical consequence is that interface parts are precision parts priced like precision parts, while extrusions are commodity parts priced per kilogramme. This is why the interface line is the one to audit when a quote looks high, and why the cheapest connector on the market is rarely the cheapest connector in the frame.
| Interface part | What it actually does | What fails if it is underspecified |
|---|---|---|
| T-nut / sliding nut | Converts groove into a threaded anchor | Spins under torque, joint never reaches preload |
| Corner bracket | Carries the moment at a 90° node | Frame racks; diagonals drift out of square |
| End cap | Closes the section, covers a cut edge | Debris ingress, snag point, exposed burr |
| Connecting plate | Splices two sections along one axis | Visible step at the joint, local bending hinge |
| Anchor / foot | Transfers load to the floor and levels it | Rock, uneven leg load, bolt pull-out |
SKU convergence: how many sections does one project really need
Every additional section profile in a project is a new line in the bill of materials, a new minimum order quantity to satisfy, and a new item that can be out of stock when the build starts. Teams that draw freely end up with nine sections; teams that converge end up with three, and the second team builds faster and cheaper for reasons that have nothing to do with the price per metre.
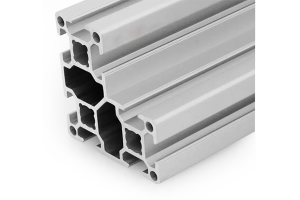
The convergence rule that works in practice is to pick one structural section for the load path and one light section for everything that only has to hold a panel. For most industrial frames that means a single 40x40 four-slot section as the spine and a 40x40 single-slot or a 20x20 section for panel retainers and cable runs.
STEP 1
Fix the load path first. Choose the section that carries bending, and commit to it for the whole spine.
STEP 2
Add one light section. Panel retainers, cable trays and sensor brackets do not need the spine section.
STEP 3
Reuse the spine for bracing. Diagonals cut from the same section avoid a fourth SKU.
STEP 4
Audit the node count. Every node you remove removes a connector and four fasteners.
Converging also protects the second build. A project that used three sections can be extended two years later from leftover stock. A project that used nine cannot, and the extension turns into a fresh purchase with a fresh minimum quantity.
The rebuild penalty nobody prices
The strongest argument for modular framing is that it can be changed. The strongest argument against it is what a change actually costs. When a frame is cut down, extended or reconfigured, the extrusions survive and most of the interface hardware does not.
Cut ends are the first casualty: a shortened member needs a new end cap and often a new machined hole. Reused T-nuts have already been torqued once, and a nut that has been seated and removed has lost part of its holding margin. Corner brackets that were bent to fit a specific geometry are not reusable at all. In practice the reuse rate on interface hardware across a rebuild sits well below half, while the reuse rate on extrusions is high.
This is the honest way to evaluate the system. If the frame will be modified at least once during its life, the interface premium buys real optionality and it is worth paying. If the design is frozen, the volume is stable and the frame will never be touched again, that premium buys nothing and a welded assembly or a dedicated extrusion is the better decision.
- The layout will change within the machine’s life
- Build time matters more than unit cost
- You need to ship a flat-pack and assemble on site
- Volumes are low to medium and mixed
- The frame carries panels, doors or guards that get re-specified
- The design is frozen and will not be revised
- Volume is high enough to amortise a die or a jig
- The node count is so high that hardware dominates the bill
- Vibration is severe and every bolted node is a risk
- Weight or envelope is tightly constrained
What to specify before you ask for a quote
Most quotation delays on modular systems are not supplier delays. They are the supplier waiting for a decision the buyer has not made yet — usually the series, the slot geometry or the surface treatment. Nine decisions, taken before the enquiry goes out, remove almost all of the back-and-forth.
RFQ checklist — modular aluminium framing
Send these nine items with the drawing and the quote comes back in one pass:
- Series and section — 20, 30, 40 or 45, with the exact external dimension.
- Slot geometry — groove width and mouth width, because this decides which hardware fits.
- Wall thickness or weight target — state kg/m if you have it; it is more reliable than a thickness callout.
- Alloy and temper — 6063-T5 for most framing, 6061 where strength or machining matters.
- Surface treatment — mill, anodised with a stated micron class, or powder coated, and state whether grooves are masked.
- Cut lengths and tolerances — per-piece length list, plus the cut tolerance you will accept.
- Machining — end tapping, counterbores, access holes; every operation is a separate cost line.
- Hardware scope — state whether connectors are included, and to what count per node.
- Quantity and packaging — first build plus the spares you will want on the second build.
Add the expected annual repeat quantity. It changes both the tooling decision and the unit price, and it is the single most commonly omitted line.
Four ways a modular frame quote goes wrong
Acceptance checks on delivery
- Count hardware against the node count on the drawing, not against the packing list.
- Test-fit one nut of every type into an anodised sample before unpacking the rest.
- Check cut lengths against the list with a tape, not against the label.
- Verify the temper and alloy marking on the bundle tag matches the order.
- Confirm the anodising micron class on the inspection sheet where one was specified.
Related on this site
- PG40 40 x 40 four-slot heavy strut profile— the section most often used as a modular spine
- Die cast bracket for 20 to 50 series— the connector class that carries a real moment at the node
- Connecting elements category— the interface hardware range
- How to choose an aluminium extrusion profile— the three decisions behind any section choice
Terms used in this article
- Node
- Any point where two or more members meet and are joined. Each node consumes connectors and fasteners.
- Interface hardware
- The connectors, nuts, bolts, plates and caps that join extrusions, as distinct from the extrusions themselves.
- SKU convergence
- Deliberately limiting a project to the smallest number of distinct section profiles that can do the job.
- Groove / mouth width
- The internal slot width and the narrower opening at the section face. Hardware is sized to both.
- Groove masking
- Protecting the slot from anodising so that the as-extruded fit is preserved.
Questions buyers ask
Is modular framing actually cheaper than welded steel?
On material alone, usually no. On total installed cost for a one-off or low-volume frame, usually yes, because the engineering and fitting hours are far lower and the frame can be corrected without cutting it apart. The crossover moves with volume and with how many times the design changes.
Why do two quotes for the same drawing differ so much?
Almost always the hardware. One supplier counted the nodes and priced every connector; the other priced the extrusions and estimated the rest. Ask both to state the connector count per node type and the difference usually disappears or becomes explainable.
Can I mix series in one frame?
Yes, and it is often sensible, but the slot geometry must match or you inherit two hardware inventories. Mixing a 40 series spine with a 20 series panel frame is common; mixing two suppliers’ versions of “40 series” is where problems start.
How much spare hardware should I order?
For a first build, order 5–10% spare nuts and bolts and at least one spare of each connector type. Nuts and bolts are consumable in a way extrusions are not, and a missing connector stops a build while a missing metre of profile rarely does.
Does anodising change what fits in the slot?
It can. The layer builds on the groove faces and eats clearance. Reputable suppliers mask grooves or tolerance the section for the coating. Test-fit hardware on an anodised sample before committing to a full build.
Send the drawing, get the node count back
We quote extrusion, hardware and machining as separate lines so you can see where the money goes. Send a sketch or a cut list and we will return a counted hardware schedule with it.
Request a quoteRelated reading
Twelve more engineering notes from this blog, picked for this article — plus every category below.
 Materials and EngineeringAluminium Extrusion Section Design: What Each Feature on the Drawing Costs You
 ApplicationsAluminium Greenhouse Profiles: A Snow Load Problem With a Condensation Problem
 Engineering DesignExtruded vs Cast Aluminium: Stronger in One Direction, Not in All of Them
 Engineering DesignCut-to-Length, Drilling and Tapping: What Fabrication Adds
 Engineering DesignAluminium Extrusion Capacity: What a Factory Can Actually Deliver
 Engineering DesignAluminium Profile Max Span: Deflection Table by Section
 Engineering DesignMetric vs Imperial T-Slot Profiles: How to Test Compatibility Before You Order
 Sourcing and ProcurementAluminium Extrusion Price per kg in 2026 (China FOB)
 ApplicationsAluminium Profile Fish Tank Frames: Glass Load, Salt Water, and the Alloy Question
 Materials and EngineeringAnodised vs Powder Coated Aluminium Profiles: A Specification Guide for European Buyers
 Quality and InspectionAluminium Profile Finishes: Choose by Failure Mode, Not by Process Name
 Quality and InspectionEuropean Anodised Aluminium Specification: What Should a Purchase Order Contain?
