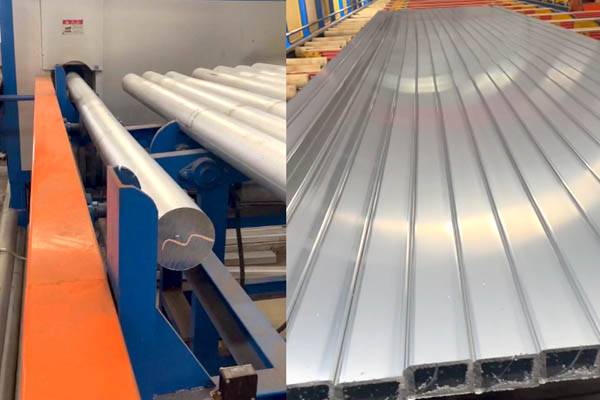
Every sourcing guide frames this as a binary: buy from the factory, or buy from a trading company. The framing is tidy and it is wrong. In the aluminium extrusion trade, the great majority of suppliers sit somewhere between those two poles, and the position they occupy determines almost everything that matters commercially — who controls the die, who can change a specification, who carries the quality risk, and who is able to tell you the truth about a delivery date.
The reason the binary framing persists is that it suits the party asking the question. A factory wants you to believe that buying anywhere else is paying a middleman for nothing. A trading company wants you to believe that factories cannot communicate or manage a complex order. Both are describing a real advantage and both are omitting the corresponding cost. A procurement director’s job is to price both honestly.
This guide is written for the person who signs the supply agreement and owns the consequences: the procurement director or supply chain manager setting up an aluminium profile category. It sets out the supplier archetypes that actually exist, eight checks that establish what a supplier genuinely is, a total cost of ownership model with worked numbers, a weighted scorecard, a two-day audit itinerary, the red flags worth walking away over, and the contract terms that prevent the disputes this industry produces most often.
What you are actually buying
One principle is worth stating before any of the detail, because it resolves most of the arguments that follow. You are not buying aluminium profiles. You are buying a supply relationship that has to survive a specification change, a quality failure, a currency movement and a schedule slip. A supplier who is cheap and cannot absorb any of those events is not cheap. A supplier who is expensive and absorbs all of them may still be the better buy. Price the relationship, not the tonne.
Quick answer
Nine points that decide the sourcing decision
Items 2 and 3 are the analytical core. Item 5 is the one that generates the most disputes, and item 9 is the one that determines whether a bad year is an inconvenience or a crisis.
There are four archetypes, not two A pure extruder with no secondary processing, an integrated manufacturer with extrusion plus machining and finishing, a group with equity in several plants, and a pure agent. Each has a different cost structure and a different failure mode.
Establish what the supplier is before you price what they offer Eight checks do this, and every one is independently verifiable: business scope, emission permit, press tonnage and count, anodising tank length, die ownership, electricity consumption against claimed output, export records, and whether the quality certificate actually covers the site you are buying from.
A 5 to 15 percent unit price saving is not a saving until you have priced the rest Inventory carrying cost, quality failure cost and management cost frequently exceed the unit price difference. In the worked example below, an 8.8 percent unit saving becomes a small net loss once the other three lines are included.
Lead time is a cost, not a service level A longer lead time means more safety stock, and safety stock has a carrying cost of roughly 15 to 25 percent of its value per year. A supplier who is 20 days slower is asking you to fund that difference.
The die is the real question Who owns the die, who can move it, who pays for its maintenance, and what happens to it if the relationship ends. This is the single most common source of disputes in Chinese aluminium profile sourcing and it is settled entirely by paperwork you either have or do not.
Quality cost is PPM multiplied by consequence, not PPM alone A defect rate means nothing without the cost of a defect. A 3,000 PPM rate on a part that costs 40 dollars to rework is a different supplier from the same rate on a part whose failure stops a line.
Score the supplier, do not rank them by instinct A weighted scorecard with published weights forces the trade-offs into the open. Six dimensions, adjustable weights, a documented score. It also makes the decision defensible to your own organisation.
Audit in two days, with a written itinerary One day of documents and extrusion, one day of finishing, machining and quality. A visit without an itinerary is a tour, and a tour produces a brochure.
Single sourcing is the risk, not the strategy A primary supplier at 70 to 80 percent, a qualified second source, and a trader for small or multi-category orders is the configuration that survives a disruption. Concentration is a cost decision made in advance of the event that punishes it.
Landscape
The four supplier archetypes that actually exist
Before scoring a supplier, establish which of these four they are. The distinction is not about honesty; all four are legitimate businesses. It is about which capabilities are inside the supplier’s control and which are subcontracted, because that is what determines who can fix a problem and how quickly.
| Archetype | What they control | Cost structure | Where they fail |
|---|---|---|---|
| Pure extruder | Presses, dies, heat treatment, cutting. Usually no machining and no finishing in-house. | Lowest conversion cost. Sells by the tonne with a narrow service envelope. | Cannot deliver a finished component. Any machining, anodising or assembly is subcontracted, so the supplier cannot control the quality of the operations that most often cause rejection. |
| Integrated manufacturer | Extrusion plus in-house machining, anodising or coating, and often assembly and packaging. | Higher conversion cost, but one organisation owns the whole process and the whole quality record. | Capacity is finite and the finishing lines are the bottleneck. A busy anodising line becomes the lead-time constraint for every order in the plant. |
| Group with equity in multiple plants | A holding structure with part-ownership of several extrusion and finishing facilities, plus its own sales and engineering function. | Between the two. Flexible capacity, and the ability to route an order to whichever plant has capacity. | Quality consistency across the group’s plants is the risk. The sample you approved and the plant that runs your production order may not be the same site. |
| Agent or pure trader | Commercial relationships, documentation, logistics and sometimes consolidation across categories. No plant of their own. | Adds a margin, and in exchange absorbs coordination and risk. | Cannot control quality or schedule directly. The failure mode is transparency: when something goes wrong, the root cause is one step further away than the person reporting it. |
The practical consequence of this table is that the question to ask a supplier is not “are you a factory?” but “which operations are in your own buildings, and for the ones that are not, who does them and under what agreement?” A supplier who answers that precisely is more useful than one who answers the first question with a yes.
There is a second dimension that the archetype table does not capture and that matters at least as much: product focus. A plant running standard catalogue profiles from stock dies behaves completely differently from a plant running custom dies to order. The first can ship in days and will resist your customisation because it disrupts a stock business. The second can produce exactly what you designed and will make you wait six weeks and pay for a die. Both are viable; neither is a substitute for the other, and a supplier who claims to be excellent at both is usually excellent at one.
Verification
Eight checks that establish what a supplier really is
Every check below can be completed without the supplier’s cooperation beyond supplying documents, and several can be completed without their cooperation at all. That independence is the point: a verification step that depends entirely on the supplier’s own description of itself is not a verification step.
Business scope on the registration record
The registered scope of business tells you whether the entity is licensed to manufacture or only to trade. Look for manufacturing and processing activities in the scope, and check that the registered address matches the site you intend to audit. A supplier whose registration is a trading scope at an office address is a trader, whatever the website says.
Environmental permit, which in this industry is unusually informative
Extrusion, anodising and coating are regulated activities with environmental requirements attached, and those permits are tied to a specific site and a specific process list. An anodising line without a corresponding permit is either not running or not compliant, and both are reasons to look elsewhere. This check is more reliable than a factory photograph.
Press tonnage and press count
Tonnage determines the maximum cross-section the plant can produce and, combined with the number of presses, the realistic monthly output. Ask for the press list with tonnage and age, and look at the presses during the audit. A plant claiming heavy-section capability without a large press is describing someone else’s plant.
Anodising tank length, if finishing is claimed
The tank length sets the longest component the line can process, and it is visible on a walk-through. This single dimension often decides whether a supplier can actually handle your longest profiles, and it is a claim that cannot be fudged in a catalogue.
Die inventory and die ownership
Ask for the die list with ownership status and the number of dies held on behalf of customers. A plant with a large library of customer-owned dies is a plant that has a functioning custom-die business. A plant with no die list is either not doing custom work or not tracking it, and both matter.
Electricity consumption against claimed output
Extrusion is energy-intensive, and consumption per tonne is a narrow band for a given technology. A plant claiming an output that its metered consumption cannot support is either overstating capacity or outsourcing the work. This cross-check is rarely performed and rarely fails to be interesting.
Export records
Ask for a sample of customs declarations or bills of lading from the past year, and check the shipper and consignee against what you have been told. Independent trade data can corroborate this. A supplier who claims to export to Europe and cannot produce a single shipping document for the region is telling you something.
Whether the quality certificate covers the site you are buying from
A quality management certificate is issued to a legal entity at a specific address, with a defined scope. Check the certificate against the site and the processes you are actually buying. A group certificate that covers a parent entity does not automatically cover the plant that will run your order, and the scope statement is where that is decided.
The address on the certificate
One check is worth repeating because it is the most frequently skipped and the most frequently consequential: the certificate address. Buyers routinely accept a scanned quality certificate as evidence that a supplier is certified, without reading which entity and which site it applies to. In a group structure this can mean that the audited and certified site is not the site that produces your order. If your own quality system or your customer’s requires a certified supplier, the certificate has to match the manufacturing location, and that is a five-minute check.
Economics
Pricing the difference properly: a total cost of ownership model
The unit price is one line in a calculation with five. The reason the factory-versus-trader debate never resolves is that both sides argue about the first line and neither prices the other four. Here is the model, followed by a worked example using realistic numbers.
TCO = (Unit price × Annual volume)
+ Die and tooling amortisation
+ Freight, duty and clearance
+ Inventory carrying cost
+ Quality failure cost
+ Management and communication cost
+ Switching cost, annualised
Each line has a defensible way of being estimated, and all six should be estimated before a supplier is selected. The three that buyers most often leave at zero — inventory, quality failure and management — are the three that most often reverse the decision.
Worked example: the saving that disappears
The numbers below are illustrative but internally consistent, and the shape of the result is the point. A buyer compares two suppliers for an annual requirement of 120 tonnes of a machined profile at roughly 1.5 kg per piece, which is 80,000 pieces per year.
| Cost line | Integrated manufacturer | Trader | Difference |
|---|---|---|---|
| Unit price | 3,200 per tonne | 3,480 per tonne | Trader is 280 per tonne higher |
| Annual material cost (120 t) | 384,000 | 417,600 | 33,600 in favour of the manufacturer |
| Lead time and safety stock | 45 days lead time; 60 days of safety stock required | 25 days lead time; 30 days of safety stock required | 30 days of additional stock at the manufacturer |
| Inventory carrying cost at 20 percent | About 6,300 per year on the additional stock | Baseline | 6,300 in favour of the trader |
| Quality failure cost | 8,000 PPM → 640 defects × 45 per defect = 28,800 | 3,000 PPM → 240 defects × 45 per defect = 10,800 | 18,000 in favour of the trader |
| Management and communication | Approximately 200 hours per year = 12,000 | Approximately 60 hours per year = 3,600 | 8,400 in favour of the trader |
| Net position | 384,000 + 6,300 + 28,800 + 12,000 = 431,100 | 417,600 + 0 + 10,800 + 3,600 = 432,000 | Trader ahead by about 900 |
The manufacturer is 8.8 percent cheaper per tonne and slightly more expensive in total. The unit price advantage of 33,600 is more than consumed by 6,300 of extra inventory, 18,000 of extra quality failure and 8,400 of extra internal management time. Nothing in this calculation is exotic and every line is estimable before the order is placed — which is exactly why leaving them out is a choice rather than an oversight.
The model is a negotiating instrument
Two things follow from the example, and both are more useful than the conclusion. First, the answer is sensitive to the inputs: change the defect cost from 45 to 90 and the manufacturer becomes clearly worse; change the carrying rate from 20 percent to 8 percent and the manufacturer wins. The model does not produce a universal answer, it produces your answer — which is the reason to build it rather than borrow someone else’s opinion. Second, and more important commercially, the model shows you what to negotiate. The 8,000 PPM figure and the 45-day lead time are the manufacturer’s weaknesses, and both are negotiable in a way that the unit price is not.
Selection
A weighted scorecard, with weights you set
A scorecard is useful for two reasons that have nothing to do with arithmetic. It forces the trade-offs into the open before the preference forms, and it produces a decision that can be explained to the rest of the organisation. The weights below are a reasonable starting point for an industrial aluminium profile category; change them to reflect your business, and publish the change.
| Dimension | Weight | What it measures | Evidence to score against |
|---|---|---|---|
| Manufacturing capability | 25 | Press tonnage and count, finishing line capability and length, machining capacity, inspection equipment, and whether the operations you need are in-house | Equipment list, on-site observation, tank length, machine count |
| Quality system | 20 | Certification that covers the site, process control, traceability, first-article and PPAP capability, calibration records, non-conforming material control | Certificate and scope, calibration log, sample quality record, traceability exercise during the audit |
| Delivery and flexibility | 15 | Lead time, minimum order quantity, ability to handle expedited orders, stock policy for standard items, response to a schedule change | Quoted lead time, MOQ, observed finished-goods stock, a test request for an expedited order |
| Commercial transparency | 15 | Clarity of quotation, alloy and temper stated, die ownership terms, price adjustment mechanism, willingness to disclose who performs subcontracted operations | Written quotation, die agreement, price adjustment clause |
| Engineering support | 15 | Drawing review and design-for-manufacture feedback, tolerance advice, sample turnaround, technical response time without an intermediary | A live test: send a drawing with a deliberate question and time the response |
| Compliance and stability | 10 | Environmental permits, restricted substances declarations, financial health, length of trading history, export record | Permit, declaration, registration and trade records, financial statements if available |
Score each dimension out of its weight, sum to 100, and record the evidence beside each score. The rule that makes the exercise work is that a score without evidence is not permitted. If you cannot point at a document or an observation that supports the number, the number is a preference and should be left blank until it is not.
Two practical notes on using it. First, run the scorecard before the price negotiation, not after. A scorecard completed with the price already known tends to produce scores that justify the price. Second, keep the scorecard current rather than re-running it from scratch at each review; the useful signal is the direction of travel, and a supplier who has slipped from 78 to 64 over eighteen months is telling you something that a single snapshot cannot.
On site
The two-day audit itinerary
A factory visit without an itinerary is a tour, and a tour produces a brochure. The itinerary below is organised so that each session has a specific question to answer, a specific thing to look at, and a specific red flag to watch for. The order matters: documents first, so that what you see on the floor can be compared against what you were told.
| Session | Ask for | Look at | Red flag |
|---|---|---|---|
| Day 1 morning: opening meeting and documents | Registration record and business scope, environmental permit, quality certificate and its scope, press and equipment list, die list with ownership, calibration schedule | Whether the certificate address matches the site, whether the permit covers anodising or coating, whether the die list names customer-owned dies | A certificate for a different address; a finishing process claimed with no permit for it; a die list that does not exist |
| Day 1 afternoon: extrusion and heat treatment | Press log for the current week, output figures, scrap rate, billet supplier and alloy certificates | Press tonnage against the equipment list, die storage and identification, ageing ovens and their temperature records, billet stock with alloy markings, scrap segregation | Press tonnage lower than claimed; dies stored loose and unlabelled; temperature records not kept; unidentified billet stock |
| Day 2 morning: finishing and machining | Anodising or coating process parameters, film thickness records, sealing test results, pre-treatment chemistry records, machining first-article records | Anodising tank length against your longest profile, film thickness gauge and its calibration, coating line and oven, CNC machines and their condition, work instructions at the machines | Film thickness reported as an average only; gauge out of calibration; no sealing test; work instructions absent or outdated |
| Day 2 afternoon: quality, warehouse and close-out | Calibration records for measuring equipment, non-conforming material register, customer complaint log, traceability record for a recent order | The laboratory and its equipment, the non-conforming material cage, finished goods and their identification, packaging against your requirement, a live traceability exercise | Non-conforming material mixed with good stock; traceability that cannot be demonstrated on demand; packaging that will not survive the journey |
The traceability exercise on the second afternoon is the single most informative hour of the visit. Take the identification number from a finished component in the warehouse and ask the supplier to show you the production record, the material certificate, the heat treatment record and the inspection result for that specific item. A supplier who can do this in ten minutes runs a system. A supplier who cannot is relying on you not asking.
Screening
Twenty red flags worth walking away over
These are observable signals rather than conclusions. Any one of them can have an innocent explanation; three or four together describe a supplier whose problems you will inherit. They are ordered roughly by how much they cost to discover late.
Two of these deserve a comment because they are commonly dismissed as commercial rather than technical. The first is the absence of a metal price index link. Aluminium is the dominant input cost in this category, and a supplier quoting a fixed price for twelve months is either pricing in a large risk premium or planning to renegotiate the moment the market moves. A published index with an agreed formula is better for both parties. The second is the refusal of a third-party inspection clause, which is not a technical capability question at all: it is a question about whether the supplier believes its own output will pass.
Agreement
The contract terms that prevent the usual disputes
In this category, a small number of clauses prevent a large proportion of the disagreements that arise. None of them is unusual and all of them are cheaper to negotiate before the first order than after the first failure.
The clause that pays for itself
One clause deserves emphasis beyond its position in the list. If your design depends on a customer-owned die, and the die ownership is not documented, then in practical terms you do not own the die. The supplier has possession, possibly the original drawings, and the working relationship with the press that runs it. Recovering a die from an unwilling supplier is slow, expensive and sometimes impossible, and it happens to buyers who assumed that paying the die invoice was sufficient. Get the ownership in the agreement, get a die identification number, and photograph the die the first time you visit.
Portfolio
The configuration that actually works
Procurement organisations that handle this category well do not choose between a factory and a trader. They run a small portfolio, with each position assigned a role. The configuration below is the one that most often survives contact with a real year.
Primary supplier: 70 to 80 percent of volume
An integrated or group manufacturer with the capability to cover your main products, a documented die arrangement and a quality system that covers the site. This is where you invest in relationship, in engineering exchange and in joint improvement, because the leverage is largest here and the switching cost is highest.
Qualified second source: 20 to 30 percent
A second manufacturer, deliberately kept qualified with a modest but continuous volume. The purpose is not price competition alone; it is that a second source which has not run your part for two years is not a second source, it is a new supplier you will have to qualify under pressure. Keep the volume flowing.
A trader for small, mixed or urgent orders
A trading partner is genuinely the better answer for a small order spanning several categories, for an urgent requirement that a plant cannot schedule, or for a component you do not want to open a die for. Paying the margin here is rational, provided you are paying it knowingly rather than being surprised by it.
A documented interface standard
Whatever the portfolio, the technical interface has to be frozen. One drawing, one set of tolerances, one finish class, applied to every supplier in the portfolio. A multi-supplier strategy without a frozen interface produces parts that fit individually and not together.
An annual review against the scorecard
Score every supplier on the same dimensions each year, with the same evidence rules, and review the direction of travel rather than the absolute number. A supplier slipping in two dimensions is a conversation; a supplier slipping in four is a sourcing project.
A costed continuity plan
Know in advance what happens if the primary supplier stops shipping: which products the second source can already make, what the lead time to ramp is, and what the inventory position would need to be. A plan written after the event is a negotiation conducted from a weak position.
The failure mode of over-diversification
There is a version of this that goes wrong and is worth naming. Some organisations respond to supplier risk by spreading volume thinly across many suppliers, on the reasoning that no single failure can hurt them. The result is usually the opposite: no supplier sees enough volume to invest in the relationship, every supplier is at the bottom of its priority list, quality varies because nobody is running the same process, and the administrative burden grows with every supplier added. Concentration and dispersion are both risks; the workable position is a small number of suppliers with clearly assigned roles and enough volume each to matter.
FAQ
Frequently asked questions
Audit the product record, not the brochure
What a factory’s own data looks like when you open it
A supplier audit is easier when the supplier publishes the same numbers you would ask for on site: material, tolerance, inspection routine, packing and lead time. That is what the entries below contain.
Building a supplier shortlist for profiles?
We will answer the eight verification questions in writing — press list, tank length, die register, permits, certificate scope — before you travel. If you would rather audit us first, send the itinerary and we will book the two days.
Related reading
Twelve more engineering notes from this blog, picked for this article — plus every category below.
 Sourcing and ProcurementAluminium Profile Quote: What Changes the Number by Quantity
 Engineering DesignModular Aluminium Components: Where the System Saves Money and Where It Costs You
 Quality and InspectionHow to Choose (and Audit) an Aluminium Extrusion Supplier
 Materials and EngineeringIndustrial Aluminium Extrusion: Five Advantages and the Conditions Attached to Each
 Engineering DesignCross-Brand T-Slot Compatibility: Interchangeability Is a Hardware Question
 Engineering DesignStandard vs Custom Aluminium Extrusion: The Break-Even Calculation
 Quality and InspectionSampling and First Article Approval for Aluminium Extrusion
 Engineering DesignWhich Profile Size for Your Application: A Selection Guide
 Engineering Design4080 vs 4545 Aluminium Profile: Which for Your Frame
 Engineering DesignAluminium Profile Standard Sizes: How the Series Matrix Actually Works
 Quality and InspectionAluminium Profile Finishes: Choose by Failure Mode, Not by Process Name
 ApplicationsAluminium Profiles for Automation Equipment Frames: Design From the Assembly Floor
